Sistema de seguridad alimentaria HACCP para la fabricación de copos de patata
Control preventivo de riesgos a lo largo de todo el proceso de producción de copos de patata
La seguridad alimentaria no se consigue únicamente mediante la inspección del producto final, sino que forma parte de cada una de las etapas del proceso de fabricación.
En Copos de patata HJ, nuestro sistema de producción de copos de patata se ha diseñado siguiendo los principios de Análisis de Peligros y Puntos Críticos de Control (HACCP), una metodología de seguridad alimentaria preventiva reconocida internacionalmente y utilizada en todo el sector alimentario mundial.
En lugar de basarnos únicamente en los análisis de laboratorio tras la producción, nuestro programa de HACCP se centra en identificar los posibles riesgos antes de que se produzcan, establecer controles preventivos, supervisar de forma continua los parámetros operativos críticos, documentar cada lote de producción y aplicar medidas correctivas siempre que se detecten desviaciones.
Desde el momento en que las patatas frescas llegan a nuestras instalaciones de procesamiento hasta que los copos de patata terminados se envasan y se preparan para su envío, cada fase se lleva a cabo siguiendo procedimientos operativos documentados, diseñados para minimizar los riesgos biológicos, físicos y químicos, al tiempo que se mantiene la calidad, la uniformidad y la trazabilidad del producto.
El proceso de fabricación integra la inspección de materias primas, los equipos de procesamiento automatizado, la validación del tratamiento térmico, la gestión de la higiene, la separación magnética, la detección de metales y la identificación de lotes en un sistema integral de gestión de la seguridad alimentaria que da soporte a fabricantes internacionales de alimentos, distribuidores de ingredientes y empresas de procesamiento industrial de alimentos.
Por qué el sistema HACCP es esencial para la producción de copos de patata
Los copos de patata deshidratados se producen mediante un complejo proceso de fabricación que incluye la gestión del agua, el tratamiento con vapor, la cocción, el secado, el transporte mecánico, la trituración y el envasado. Cada etapa plantea diferentes aspectos relacionados con la seguridad alimentaria que requieren una supervisión y un control sistemáticos.
A diferencia de muchos ingredientes de alimentos secos, que se someten a un procesamiento limitado, los copos de patata pasan por múltiples operaciones térmicas y mecánicas antes de convertirse en un producto de larga conservación. Los cambios en la temperatura, el contenido de humedad, el funcionamiento de los equipos y la manipulación del producto deben gestionarse cuidadosamente para garantizar la seguridad alimentaria y un rendimiento constante del producto.
Un sistema preventivo de HACCP ayuda a los fabricantes a controlar los riesgos antes de que afecten a los productos terminados, mediante la identificación de:
- Posibles riesgos biológicos asociados a las materias primas agrícolas
- Peligros físicos, como piedras, fragmentos metálicos y materiales extraños
- Riesgos químicos relacionados con los coadyuvantes tecnológicos autorizados y los procedimientos de higiene
- Riesgos de contaminación relacionados con los equipos
- Desviaciones en los procesos que podrían afectar a la calidad del producto o a la seguridad alimentaria
Mediante un seguimiento continuo, procedimientos operativos documentados, la formación de los empleados y actividades de verificación, el sistema HACCP transforma la seguridad alimentaria, pasando de ser una inspección reactiva a una gestión proactiva de los procesos.
Nuestra filosofía sobre el sistema HACCP
En HJ Potato Flakes, el sistema HACCP se aplica como parte de un sistema integrado de gestión de la fabricación, y no como un programa de calidad aislado.
La seguridad alimentaria comienza con la selección cuidadosa de las patatas crudas y se mantiene a lo largo de todas las fases de producción, incluyendo el lavado, el pelado, el escaldado, la cocción, el secado, la trituración, el envasado, el almacenamiento y el envío.
Cada fase de producción cuenta con parámetros operativos definidos, requisitos de control, procedimientos de higiene, calendarios de mantenimiento de los equipos y requisitos de documentación que, en conjunto, contribuyen a reducir el riesgo a lo largo de todo el proceso de fabricación.
Este enfoque preventivo ofrece varias ventajas importantes:
- Calidad constante del producto entre los distintos lotes de producción
- Mejor control de la contaminación física
- Contenido de humedad estable y rendimiento del producto
- Trazabilidad completa de los lotes
- Documentación de producción fiable
- Mayor confianza para los fabricantes de alimentos y los clientes industriales
Objetivos del sistema HACCP
Entre los objetivos principales de nuestro sistema HACCP se incluyen:
Proteger la seguridad alimentaria de los consumidores
Identificar y controlar los posibles riesgos antes de que se introduzcan en los productos terminados mediante controles preventivos en la fabricación, en lugar de basarse únicamente en la inspección de los productos terminados.
Mantener una calidad de fabricación constante
Establecer parámetros de producción validados para cada fase del proceso con el fin de garantizar unas características uniformes del producto, entre ellas la humedad, el tamaño de las partículas, el color, la textura y el comportamiento de rehidratación.
Prevenir la contaminación por materiales extraños
Aplicar múltiples medidas de control independientes —entre ellas, el lavado, la inspección manual, la separación magnética y la detección final de metales— para minimizar los riesgos de contaminación física.
Cumplimiento de los requisitos internacionales en materia de fabricación de productos alimenticios
Aplicar procedimientos de producción estandarizados que se ajusten a los principios de gestión de la seguridad alimentaria reconocidos internacionalmente y a los programas de cualificación de proveedores de los clientes.
Garantizar la trazabilidad completa del producto
Llevar registros de producción exhaustivos que permitan rastrear cada lote de producto terminado, desde los registros de procesamiento hasta las materias primas recibidas.
Ámbito de aplicación del sistema HACCP
Nuestro programa de HACCP abarca todo el proceso de fabricación, desde la recepción de la patata en bruto hasta el almacenamiento del producto terminado.
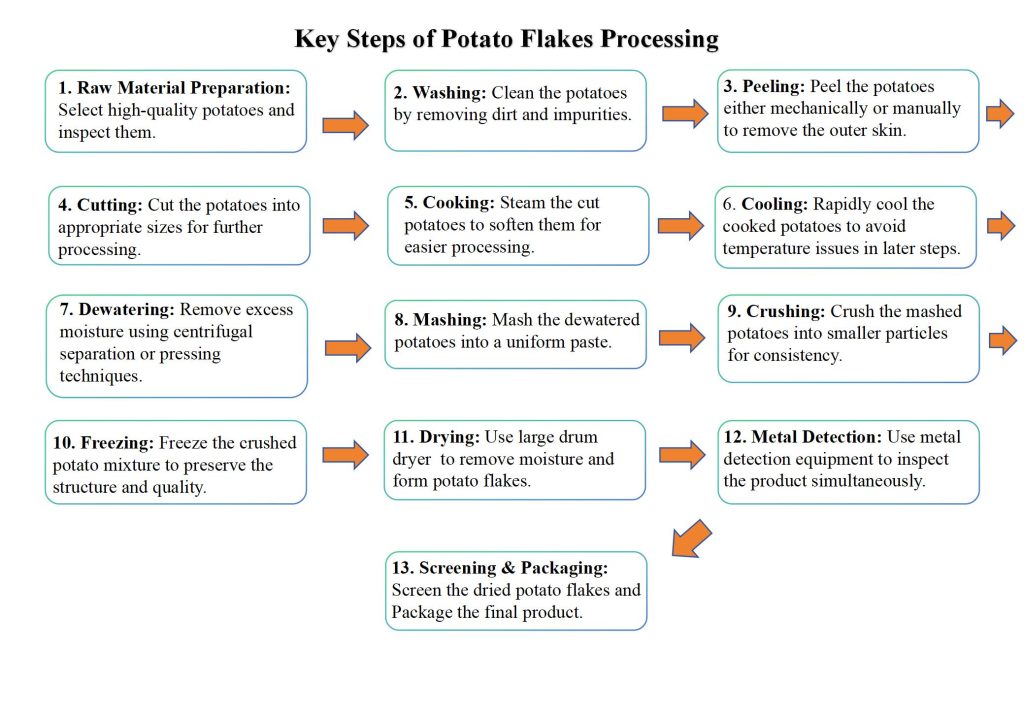
| Fase de fabricación | Control primario de la seguridad alimentaria |
|---|---|
| Recepción de materias primas | Aprobación de proveedores e inspección de entrada |
| Almacenamiento de patatas | Condiciones de almacenamiento controladas |
| Extracción y lavado de piedras | Eliminación de tierra, piedras y materiales extraños |
| Exfoliación al vapor | Proceso de pelado térmico controlado |
| Exfoliación con cepillo | Eliminación de restos de cáscara |
| Después del lavado | Limpieza de superficies y gestión del agua de recirculación |
| Inspección manual | Eliminación de patatas defectuosas y materiales extraños |
| Corte hidráulico | Preparación uniforme del producto |
| Escaldado | Inactivación enzimática y estabilización del proceso |
| Refrigeración | Reducción controlada de la temperatura del producto |
| Cocina | Procesamiento térmico completo |
| Maceración | Procesamiento mecánico controlado |
| Secado en tambor | Reducción de la humedad y estabilidad de conservación |
| Molienda y tamizado | Homogeneidad del tamaño de las partículas |
| Separación magnética | Eliminación de metales ferrosos |
| Embalaje | Protección e identificación de productos |
| Detección de metales (CCP) | Control definitivo de los riesgos físicos |
| Almacenamiento en almacén | Gestión de lotes y envío |
Cada fase de fabricación se sustenta en procedimientos operativos documentados, programas de higiene, mantenimiento de los equipos, formación de los empleados y actividades de control de calidad.
El enfoque preventivo en materia de seguridad alimentaria
Los sistemas de calidad tradicionales suelen depender en gran medida de las pruebas realizadas a los productos terminados una vez finalizada la fabricación.
Un sistema basado en el HACCP centra la atención en la prevención.
En lugar de preguntarse si un producto terminado cumple con las especificaciones tras su fabricación, el enfoque HACCP se plantea continuamente la siguiente pregunta:
- ¿Qué riesgos podrían producirse en esta fase del proceso?
- ¿Cómo se pueden prevenir estos riesgos?
- ¿Qué parámetros de funcionamiento deben supervisarse?
- ¿Qué registros demuestran el control de los procesos?
- ¿Qué medidas correctivas hay que adoptar si se producen desviaciones?
Esta filosofía preventiva se aplica en toda nuestra línea de producción de copos de patata, lo que permite gestionar la seguridad alimentaria de forma sistemática, en lugar de limitarse a realizar inspecciones al final del proceso de producción.
De la patata cruda a los copos de patata listos para el consumo
Las patatas frescas se someten a una secuencia de operaciones de procesamiento cuidadosamente controlada, diseñada para conservar las características naturales de la patata y, al mismo tiempo, obtener un ingrediente deshidratado estable y de alta calidad.
El proceso de producción incluye:
1. Recepción de materias primas:Puerta crítica 1.
Cada lote que llega de Patatas Atlantic/Shepody Se somete a un proceso de desgranado enérgico, un lavado continuo y un riguroso recorte visual para eliminar la tierra, las piedras y los frutos defectuosos antes de entrar en la línea de producción.
2. Exfoliación avanzada con vapor:Controlado por PLC.
Sometido brevemente a vapor a alta presión (0,8–1,5 MPa). La piel exterior se desprende de forma natural con una pérdida mínima de pulpa, lo que reduce rápidamente la carga microbiana superficial.
3. Blanqueado y enfriamiento validados:Inactivación enzimática.
Las rebanadas se calientan a 65–83 °C para desactivar por completo la peroxidasa y la catalasa, y a continuación enfriar rápidamente hasta ≤30 °C para fijar las cadenas de almidón y optimizar la elasticidad de la pared celular.
4. Cocción precisa y triturado suave:Preservación de la integridad celular.
Cocción al vapor controlada (92–99 °C) permite una gelatinizacion completa del almidón. El macerado suave separa las células sin que se rompan, evitando las texturas pegajosas.
5. Secado de precisión en tambor:Control de la humedad.
El puré se extiende en un 0,20–0,25 mm película fina. La presión del vapor y la velocidad del tambor se regulan para mantener la humedad final estrictamente por debajo de 9% para garantizar la estabilidad durante el almacenamiento.
6. Barreras de varias etapas contra riesgos físicos:Punto crítico de control (PCC).
Los copos atraviesan la doble capa Separadores magnéticos de ≥8.000 gauss (limpiado cada 4 horas), seguido del paso de la muestra 100% en una bolsa sellada individual a través de un dispositivo calibrado Detectores de metales (CCP).
Cada operación aporta funciones específicas relacionadas con la seguridad alimentaria, la calidad y el control de procesos que, en conjunto, conforman un sistema integral de fabricación preventiva.
Control de las materias primas y prevención de riesgos en las primeras fases
La eficacia de un sistema HACCP depende en gran medida del control de los peligros antes de que entren en la línea de producción. En la fabricación de copos de patata, la seguridad alimentaria comienza mucho antes de la cocción o el secado: empieza por la calidad de las patatas frescas que se reciben de los proveedores autorizados.
HJ Potato Flakes aplica medidas de control preventivo a lo largo de todo el proceso de recepción, almacenamiento, lavado, pelado, recorte y corte de la materia prima, con el fin de reducir los riesgos biológicos, físicos y relacionados con la calidad antes de que comience el procesamiento térmico.
Recepción de materias primas
Las bases para una producción segura de copos de patata
Las patatas frescas son la única materia prima importante que se utiliza en la fabricación de copos de patata. Dado que las patatas son un producto agrícola, existen variaciones naturales entre las distintas temporadas de cosecha, las regiones de cultivo y las condiciones de almacenamiento.
Por lo tanto, el control de entrada es el primer punto de control preventivo dentro del sistema de fabricación.
Cada entrega se evalúa según las especificaciones documentadas de las materias primas antes de pasar a la fase de producción.
Entre los aspectos que suelen inspeccionarse se incluyen:
- Variedad de patata
- Aspecto exterior
- Madurez
- Frescura
- Daños mecánicos
- Síntomas de la enfermedad
- Decoloración verde
- Materiales extraños
- Condiciones de almacenamiento
- Condiciones de transporte
Solo se admiten en el sistema de transformación las patatas que cumplen los requisitos de producción.
Los lotes que no cumplen los requisitos de las especificaciones se identifican, se aíslan y se gestionan de acuerdo con los procedimientos de calidad documentados.
Análisis de riesgos — Recepción de materias primas
| Categoría de peligro | Peligro potencial | Control preventivo |
|---|---|---|
| Biológico | Patatas podridas, moho, proliferación microbiana | Control de entrada y homologación de proveedores |
| Físico | Piedras, tierra, madera, plástico, objetos extraños | Inspección visual antes de la descarga |
| Químico | Residuos agrícolas que no cumplen las especificaciones | Programas homologados de gestión de proveedores y de ensayos |
Se mantienen registros de inspección de entrada para garantizar la trazabilidad completa de los lotes.
Almacenamiento de patatas crudas
Tras su recepción, las patatas se trasladan a las zonas de almacenamiento designadas antes de planificar la producción.
Es importante almacenarlas correctamente, ya que las patatas siguen estando biológicamente activas tras la cosecha. La temperatura, la ventilación, la humedad y la duración del almacenamiento influyen en la calidad del procesamiento.
El almacenamiento controlado ayuda a mantener:
- Contenido estable de materia seca
- Niveles adecuados de azúcares reductores
- Características de cocción uniformes
- Color uniforme de las escamas
- Menor riesgo de deterioro
La rotación de existencias se rige por procedimientos de planificación de la producción documentados, con el fin de reducir al mínimo los períodos de almacenamiento excesivos.
Eliminación de piedras y lavado primario
Eliminación de contaminantes físicos antes del procesamiento
Las patatas recién cosechadas suelen tener tierra, arena, piedras y restos del campo adheridos a su superficie.
La eliminación de estos contaminantes al inicio de la producción protege los equipos situados más adelante en el proceso y reduce los riesgos físicos que podrían llegar a las fases posteriores de procesamiento.
Las patatas se transportan a un sistema de eliminación de piedras y lavado de tipo sinfín que utiliza agua corriente.
Dado que las piedras son considerablemente más pesadas que las patatas, se depositan de forma natural en el fondo del separador y se descargan a través de la cinta transportadora de eliminación de piedras.
Las patatas pasan a la sección de lavado, donde el movimiento giratorio del agua desprende y elimina:
- Suelo
- Arena
- Piedrecitas
- Residuos vegetales
- Polvo superficial
- Materiales extraños sueltos
Un enjuague final con chorro de agua limpia aún más la superficie de la patata antes de su traslado al sistema de pelado.
Control de riesgos según el sistema HACCP durante el lavado
El lavado primario cumple varias funciones importantes en materia de seguridad alimentaria:
Reducción de los riesgos físicos
El proceso de lavado elimina los materiales que, de otro modo, podrían dañar los equipos de procesamiento o contaminar los productos terminados.
Entre ellos se incluyen:
- Piedras
- Grava
- Arena
- Terrones de tierra
- Residuos vegetales
Protección de los equipos
La entrada de materiales extraños en las peladoras a vapor, los equipos de corte o las bombas puede dañar la maquinaria o reducir la eficiencia del proceso.
La retirada temprana contribuye a mantener un funcionamiento estable de los equipos durante todo el proceso de producción.
Limpieza de las superficies
Aunque el lavado no está pensado como una etapa de eliminación de microorganismos, reduce significativamente la contaminación visible en la superficie de la patata antes del procesamiento térmico.
Gestión del agua
La calidad del agua es un factor importante que hay que tener en cuenta a lo largo de todo el proceso de elaboración de la patata.
Durante las operaciones de lavado:
- Los sistemas de circulación de agua se someten a un mantenimiento continuo.
- Se añade agua fresca para mantener la eficacia del lavado.
- Las aguas residuales se conducen al sistema de tratamiento de aguas residuales.
- El agua de proceso no entra en contacto con los productos terminados tras el secado.
Una gestión adecuada del agua contribuye tanto a la seguridad alimentaria como a la responsabilidad medioambiental.
Exfoliación al vapor
Tecnología de exfoliación térmica controlada
After washing, potatoes are transported by inclined conveyor into the steam peeling system.
Steam peeling removes potato skin quickly while minimizing loss of edible potato tissue.
Unlike mechanical abrasion alone, steam peeling briefly exposes potatoes to high-pressure steam.
The outer skin rapidly heats, softens, expands, and separates naturally from the underlying potato.
This method improves peeling efficiency while preserving yield.
Process Parameters
Typical operating conditions include:
| Parámetro | Operating Range |
|---|---|
| Steam Pressure | 0,8–1,5 MPa |
| Steam Exposure Time | 15–45 seconds |
| Control de procesos | Fully automated PLC system |
The automated control system regulates:
- Feeding time
- Steam injection
- Pressure control
- Discharge timing
This minimizes process variation between production batches.
Food Safety Contribution of Steam Peeling
Steam peeling provides several preventive food safety benefits.
Surface Microbial Reduction
High-temperature steam reduces the microbial load present on potato skins before subsequent processing.
Improved Peeling Consistency
Uniform peel removal decreases the likelihood that damaged or contaminated peel remains attached during downstream processing.
Reduced Product Loss
Because only the outer skin is softened, edible potato tissue remains largely intact, improving manufacturing efficiency while maintaining product quality.
Dry Brush Peeling
Removal of Residual Peel
After steam peeling, a small amount of peel may remain attached to the potato surface.
The potatoes therefore enter a dry brush peeling system equipped with rotating nylon brushes.
As potatoes move through the equipment:
- Gentle friction removes remaining peel.
- Surface cleaning continues.
- Loose peel fragments are separated from potatoes.
- Potatoes are cleaned on all sides before washing.
Residual peel is collected separately and transferred to designated residue handling systems.
Environmental and By-product Management
Potato peel generated during processing is collected through enclosed handling systems.
Instead of entering finished products, peel residues are directed into collection tanks before being transported for approved agricultural utilization, such as livestock feed where permitted by local regulations.
This controlled separation helps maintain production hygiene while reducing waste.
Después del lavado
Following brush peeling, potatoes undergo another washing stage.
The objectives of post-washing include:
- Removing loosened peel fragments
- Removing remaining surface residue
- Preparing potatoes for manual inspection
- Improving visibility during sorting
Inside the rotating drum washer, potatoes tumble gently while clean water sprays continuously over the product.
Water passes through filtration systems before recirculation.
Fresh water is continuously added to maintain washing effectiveness.
HACCP Controls During Post-Washing
Food safety controls include:
- Continuous water circulation
- Filtration of suspended solids
- Separation of peel residues
- Routine sanitation of equipment
- Controlled wastewater discharge
These measures reduce the transfer of contaminants into subsequent processing stages.
Manual Visual Inspection
Human Inspection Remains an Essential Food Safety Control
Although modern potato processing relies heavily on automated equipment, trained personnel continue to play an essential role in identifying defects that machines cannot always detect reliably.
Following washing, potatoes pass slowly across an inspection table where trained operators visually examine every potato.
Inspection personnel remove potatoes or potato portions showing unacceptable defects before slicing.
Defects Removed During Inspection
Operators remove:
- Green potato tissue
- Rotten potatoes
- Blackened areas
- Diseased tissue
- Potato eyes
- Daños mecánicos
- Residual peel
- Materiales extraños
Only potatoes meeting quality requirements continue into production.
Rejected material is immediately separated from acceptable product and transferred to designated waste collection areas.
Why Manual Inspection Matters
Visual inspection improves both food safety and finished product quality.
Removing defective potatoes helps:
- Improve finished product appearance
- Maintain natural potato flavor
- Reduce discoloration
- Improve processing consistency
- Prevent poor-quality raw materials from entering thermal processing
Although automated optical sorting technologies continue to evolve, trained operators remain an important component of comprehensive food safety management in many potato processing facilities.
Thermal Processing Controls: From Slicing to Mashing
After raw potatoes have been inspected, cleaned, and trimmed, the manufacturing process enters its most critical phase. This section of the production line transforms fresh potato tissue into a stable mashed potato base through carefully controlled slicing, blanching, cooling, cooking, and mashing operations.
These thermal processing stages are essential not only for product quality, but also for process consistency, enzyme control, texture development, and preparation for efficient dehydration.
Each operation is monitored using validated process parameters that help maintain consistent product performance while supporting the overall HACCP food safety system.
Corte hidráulico
Producing Uniform Potato Slices for Consistent Heat Transfer
Uniform slice thickness is one of the most important factors affecting downstream thermal processing.
If slices are too thick, heat penetration during blanching and cooking may become inconsistent. If slices are too thin, excessive cell damage and starch loss may occur, affecting mash quality and final flake performance.
To achieve consistent processing, potatoes enter a hydraulic slicing system where they are conveyed by flowing water through precision cutting blades.
Unlike conventional mechanical feeding systems, hydraulic conveying minimizes mechanical impact while ensuring a continuous and stable product flow.
The slicing system produces smooth, uniform potato slices with a typical thickness of 8–12 mm, allowing heat to penetrate evenly during subsequent blanching and cooking.
After slicing, excess process water is removed in a drum dewatering unit before the slices are transferred to the blanching system.
Food Safety and Quality Benefits of Uniform Slicing
Consistent slice dimensions provide several manufacturing advantages.
Uniform Heat Distribution
Even slice thickness allows all potato slices to receive similar thermal treatment, reducing process variation between individual pieces.
Improved Cooking Consistency
Uniform slices reach the desired internal temperature at approximately the same rate, supporting consistent starch gelatinization throughout the batch.
Reduced Mechanical Damage
Hydraulic conveying minimizes unnecessary impacts that could rupture potato cells before cooking.
Preserving cellular structure is important because intact potato cells contribute significantly to the desirable texture and rehydration performance of finished potato flakes.
Escaldado
The First Controlled Thermal Processing Stage
Blanching is one of the most scientifically important operations in potato flake manufacturing.
Although often misunderstood as simply heating potatoes, blanching performs several critical biochemical functions that directly influence the appearance, texture, flavor, and processing characteristics of the finished product.
Fresh potatoes naturally contain active enzymes, including peroxidase y catalase. If these enzymes remain active during production, they can trigger enzymatic browning, accelerate quality deterioration, and negatively affect product color during storage.
Controlled blanching inactivates these enzymes before further processing.
Typical Operating Parameters
| Process Parameter | Rango típico |
|---|---|
| Temperatura | 65–83 °C |
| Residence Time | 15–35 minutes |
| Heating Medium | Steam and hot water mixture |
The blancher is designed to move potato slices slowly through a controlled heating environment, ensuring every slice receives uniform exposure.
Scientific Functions of Blanching
Blanching contributes to both food safety and product quality through several mechanisms.
Enzyme Inactivation
The primary objective is to deactivate naturally occurring enzymes responsible for enzymatic browning and quality deterioration.
This helps preserve the light cream color expected in premium potato flakes.
Cell Structure Stabilization
Controlled heating strengthens interactions between potato cells while reducing excessive cell rupture during later processing.
Maintaining cell integrity is one of the reasons high-quality potato flakes rehydrate into mashed potatoes with a smooth, natural texture instead of becoming excessively sticky.
Partial Starch Gelatinization
Blanching begins the starch transformation process.
Controlled gelatinization prepares the potato tissue for uniform cooking without causing excessive starch leakage.
Improved Mash Characteristics
Proper blanching helps individual potato cells separate more easily during mashing, producing a fluffy mashed potato structure with improved rehydration properties.
Refrigeración
Controlled Cooling Before Final Cooking
Immediately after blanching, potato slices enter a cooling system where they are exposed to counter-current cooling water.
At first glance, cooling before cooking may appear unnecessary. However, this operation plays an important role in optimizing the physical properties of potato tissue.
Rather than simply lowering product temperature, controlled cooling modifies the internal structure of the potato to improve downstream processing.
Typical Operating Parameters
| Parámetro | Valor |
|---|---|
| Product Temperature | ≤30 °C |
| Residence Time | 15–35 minutes |
Why Cooling Improves Product Quality
Increased Cell Wall Elasticity
Gradual cooling allows cell membranes to contract naturally.
This improves the mechanical strength of potato cells before final cooking and mashing.
Reduced Free Starch
Cooling helps remove free starch released during blanching.
Lower levels of free starch reduce mash viscosity and help prevent sticky textures.
Better Rehydration Performance
Maintaining intact potato cells throughout thermal processing enables finished potato flakes to absorb water more evenly during reconstitution.
The result is mashed potatoes with improved texture and mouthfeel.
Cocina
Complete Thermal Cooking Under Controlled Steam Conditions
After cooling, potato slices enter the cooking system through an enclosed feeding arrangement that provides continuous and uniform product flow.
Cooking represents the primary thermal processing stage in potato flake manufacturing.
The objective is to cook every potato slice thoroughly while preserving as much cellular integrity as possible.
Unlike household boiling, industrial cooking systems are carefully controlled to achieve consistent heat transfer across large production volumes.
Typical Operating Parameters
| Parámetro | Operating Range |
|---|---|
| Steam Pressure | 0.3–0.4 MPa |
| Product Temperature | 92–99 °C |
| Cooking Time | 15–45 minutes |
Actual operating conditions may vary depending on potato variety, dry matter content, seasonal characteristics, and production requirements.
Objectives of Controlled Cooking
Complete Starch Gelatinization
Cooking converts potato starch into its fully gelatinized form, allowing the finished flakes to rehydrate rapidly when prepared by customers.
Uniform Softening
Consistent heating ensures that all potato slices reach the desired softness before mashing.
Uneven cooking may produce undesirable hard particles or inconsistent flake quality.
Stable Processing Conditions
Carefully controlled steam pressure and cooking time reduce batch-to-batch variation while supporting consistent product specifications.
Scientific Importance of Starch Gelatinization
Starch gelatinization is one of the key transformations occurring during potato processing.
As potato tissue is heated in the presence of moisture, starch granules absorb water and expand.
This process changes the internal structure of the potato, producing the smooth texture associated with mashed potatoes.
Proper gelatinization also improves:
- Absorción de agua
- Rehydration speed
- Consistencia del producto
- Textura final
- Estabilidad durante el procesamiento
Incomplete gelatinization may reduce product performance, while excessive heating can damage cell structure and increase stickiness.
Maintaining the correct balance is therefore essential.
Maceración
Transforming Cooked Potatoes into a Uniform Mash
After cooking, softened potato slices are transferred directly into the mashing system.
The purpose of mashing is not to pulverize the potatoes completely, but rather to separate cooked potato tissue while preserving as many intact cells as possible.
This distinction is one of the defining characteristics of premium potato flake manufacturing.
Gentle Mechanical Processing
Inside the mashing machine, a screw conveyor gradually feeds cooked potatoes through a specially designed mash screen.
The equipment operates at controlled speed to avoid unnecessary cell rupture.
Maintaining intact potato cells contributes significantly to:
- Natural mashed potato texture
- Improved mouthfeel
- Reduced stickiness
- Better water absorption after rehydration
- Consistent finished flake quality
Process Aids
During mashing, carefully controlled amounts of approved food ingredients may be incorporated to improve processing stability and finished product performance.
Typical additions include:
| Ingrediente | Primary Function |
|---|---|
| Mono- and Diglycerides | Improve texture and reduce stickiness during rehydration |
| Ácido cítrico | Helps reduce enzymatic browning and oxidation while maintaining product appearance |
These ingredients are used only within established food manufacturing specifications and are uniformly dispersed throughout the mash to ensure consistent product quality.
HACCP Considerations During Thermal Processing
The slicing, blanching, cooling, cooking, and mashing stages work together to achieve several preventive food safety objectives:
| Processing Stage | Primary HACCP Purpose |
|---|---|
| Corte hidráulico | Uniform product preparation for consistent heat transfer |
| Escaldado | Inactivación enzimática y estabilización del proceso |
| Refrigeración | Cell structure optimization and free starch reduction |
| Cocina | Complete thermal processing and starch gelatinization |
| Maceración | Controlled mechanical processing while preserving cell integrity |
Although the Critical Control Point (CCP) is established later at the metal detection stage, these thermal processing operations form the backbone of product consistency and preventive process control. Standard operating procedures, equipment monitoring, sanitation programs, and production records ensure each batch progresses through validated processing conditions before entering the drying and finishing stages.
Drying, Foreign Material Control, and Critical Control Point (CCP)
After the potatoes have been fully cooked and gently mashed, the manufacturing process enters the final transformation stage. During this phase, the moist potato mash is converted into shelf-stable potato flakes through precision drum drying, particle size control, magnetic separation, packaging, and final metal detection.
This section represents one of the most critical parts of the HACCP system because it combines product stabilization with multiple independent physical hazard control measures before the product leaves the production facility.
Rather than relying on a single inspection point, HJ Potato Flakes applies a multi-barrier contamination prevention strategy, where several independent control systems work together to minimize physical contamination risks.
Secado en tambor
Converting Fresh Potato Mash into Shelf-Stable Potato Flakes
Fresh mashed potatoes contain a high percentage of water and therefore require dehydration to achieve the stability necessary for storage and transportation.
Drum drying is a highly efficient dehydration method widely used in potato flake manufacturing because it combines rapid moisture removal with gentle handling of the potato structure.
The mashed potato is transferred from the mash holding system to the drum dryer using a controlled pressure feeding system.
A rotor pump distributes the mash evenly across the rotating drying drum as a very thin film.
Maintaining a consistent film thickness is essential for achieving uniform drying across the entire production batch.
Typical Operating Parameters
| Process Parameter | Typical Operating Range |
|---|---|
| Steam Pressure | 0.8–1.2 MPa |
| Drum Surface Temperature | 120–240°C |
| Mash Film Thickness | 0,20–0,25 mm |
| Drum Speed | Approximately 1–10 rpm |
| Finished Moisture | Typically below 9% (or customer specification) |
Production operators continuously adjust steam pressure and drum rotation speed according to product characteristics, seasonal raw material variation, and customer requirements.
This ensures stable drying performance while maintaining product consistency.
Why Moisture Control Is Critical
Moisture is one of the most important quality indicators for dehydrated potato products.
Excess moisture may reduce storage stability and increase the risk of product deterioration, while excessive drying can negatively affect texture, color, and rehydration performance.
Maintaining the target moisture level provides several important benefits.
Improved Shelf Stability
Lower moisture content limits microbial growth and helps maintain product quality during storage.
Consistent Rehydration
Uniform drying allows potato flakes to absorb water evenly during food preparation.
Product Flowability
Properly dried flakes flow more consistently during packaging and industrial food manufacturing.
Stable Transportation
Controlled moisture reduces product caking during storage and shipment.
Formation of Potato Flakes
After drying, the thin layer of dehydrated potato is gently removed from the drum surface using precision scraper blades.
Instead of producing fine powder immediately, the dried sheet naturally breaks into large flakes.
These flakes retain much of the original potato cell structure developed during previous processing stages.
Preserving this structure is one of the reasons premium potato flakes produce smooth mashed potatoes after rehydration.
Flaking, Grinding, and Particle Size Control
Producing Consistent Product Specifications
Following drum drying, the large flakes enter a controlled size reduction system.
Rather than grinding aggressively, the process gradually reduces particle size while minimizing unnecessary mechanical damage.
The production sequence includes:
- Primary flake breaking
- Vacuum conveying
- Controlled flaking
- Grinding
- Particle size classification
- Final screening
Grinding speed is adjusted according to customer specifications and desired product characteristics.
Particle Size Classification
Finished products are screened through calibrated sieves to achieve consistent particle size distribution.
Typical screening specifications range from 16 to 40 mesh, depending on customer application.
Consistent particle size contributes to:
- Mezcla homogénea
- Stable bulk density
- Improved packaging efficiency
- Consistent hydration
- Better processing performance in downstream food manufacturing
Foreign Material Control Strategy
Multiple Independent Physical Hazard Barriers
One of the strengths of our HACCP system is that physical contamination is controlled through multiple independent barriers rather than relying on a single inspection point.
Each control step reduces the possibility that foreign materials progress further through the manufacturing process.
| Production Stage | Hazard Controlled |
|---|---|
| Stone Removal | Stones, gravel, heavy foreign materials |
| Lavado | Soil and surface contaminants |
| Inspección manual | Defective potatoes and visible foreign materials |
| Tamizado | Oversized particles and processing irregularities |
| Separación magnética | Ferrous metal contamination |
| Detección de metales (CCP) | Final verification of packaged products |
This layered approach provides redundancy and significantly improves food safety reliability.
High-Strength Magnetic Separation
Continuous Ferrous Metal Removal
Following particle size classification, potato flakes pass through a double-layer magnetic separation system.
The magnetic separator is designed to continuously capture ferrous contaminants that could potentially originate from equipment wear or other processing sources.
The magnetic field strength is maintained at not less than 8,000 Gauss, providing strong magnetic attraction for ferrous particles before packaging.
Because magnetic separation operates continuously throughout production, it functions as an important preventive control before the Critical Control Point.
Magnetic Separator Verification Program
Effective magnetic separation requires regular inspection and documented maintenance.
HJ Potato Flakes implements a routine verification program that includes both equipment performance checks and cleaning procedures.
Magnetic Strength Verification
The Quality Control department verifies magnetic strength every 10 days.
If magnetic strength falls below 7,000 Gauss, the magnetic rods are replaced immediately to maintain effective contamination control.
This preventive maintenance program helps ensure consistent equipment performance throughout production.
Scheduled Cleaning Program
Magnetic rods are cleaned according to documented operating procedures.
Typical cleaning frequency includes:
- Every hour during the first three hours of production
- Every four hours during normal operation
If metal fragments larger than 3 mm are observed during cleaning, the inspection frequency is immediately increased to once every hour until normal operating conditions are restored.
This risk-based approach allows production personnel to respond quickly to abnormal equipment conditions.
Documented Cleaning Procedures
Cleaning activities follow standardized operating instructions to ensure consistency.
Typical procedures include:
- Cleaning and sanitizing hands before handling equipment
- Removing magnetic rods carefully
- Cleaning rods with approved alcohol and lint-free cloths
- Recording magnetic rod weight before and after cleaning
- Inspecting removed metal particles
- Collecting metal fragments larger than established criteria in labeled containers
- Recording production date, production shift, batch number, and operator information
- Returning cleaned magnetic rods to the production line after verification
These documented records provide objective evidence that preventive controls are functioning as intended.
Critical Control Point (CCP)
Final Metal Detection
Within the HACCP system, the finished product metal detection stage is designated as the primary Critical Control Point (CCP).
Every sealed package passes individually through a calibrated metal detector before entering finished product storage.
Unlike preventive control steps earlier in the process, the CCP serves as the final verification that packaged products meet established physical hazard requirements.
Metal Detector Performance Standards
The metal detection system is capable of identifying very small metal contaminants.
Typical detection sensitivity includes:
| Metal Type | Detection Capability |
|---|---|
| Ferrous (Fe) | ≤ 1.5 mm |
| Non-Ferrous | ≤ 2.4 mm |
| Stainless Steel (SUS) | ≤ 3.0 mm |
These sensitivity levels are verified using certified metal test pieces.
Procedimientos de control de los puntos críticos de control (CCP)
To ensure continuous effectiveness, the metal detector undergoes routine operational verification throughout production.
Verification includes:
- Functional testing every four hours
- Verification using certified ferrous, non-ferrous, and stainless steel test pieces
- Recording inspection results
- Immediate corrective action if verification fails
Only products passing metal detection are released for finished goods storage.
Corrective Actions
If the metal detector alarms or verification results fall outside established limits, production personnel follow documented corrective procedures.
These may include:
- Immediate isolation of affected products
- Identification of the production batch
- Equipment inspection
- Investigation of the root cause
- Reinspection after corrective action
- Documentation of findings before production resumes
No product is released until the cause of the deviation has been identified and appropriate corrective measures have been completed.
Why Multiple Physical Hazard Controls Matter
A common misconception is that metal detection alone ensures product safety.
In reality, effective HACCP systems rely on multiple preventive barriers working together throughout the manufacturing process.
At HJ Potato Flakes, physical hazard control begins at raw potato receiving and continues through washing, trimming, sieving, magnetic separation, and finally metal detection.
Each individual control reduces risk, while the combination of all controls provides a far higher level of protection than any single inspection point alone.
This preventive, layered approach reflects internationally recognized HACCP principles and supports the consistent production of high-quality dehydrated potato ingredients for food manufacturers worldwide.
Packaging Control, Product Traceability, Sanitation Programs, and Continuous HACCP Verification
Food safety does not end when potato flakes leave the production line. After drying and foreign material control have been completed, every production batch continues through standardized packaging, coding, traceability, storage, and verification procedures designed to maintain product integrity until shipment.
These post-processing activities are an essential part of the HACCP system because they ensure that product identity, package integrity, and production records remain accurate throughout the supply chain.
Packaging Control
Protecting Product Quality After Processing
Packaging serves as the final physical barrier protecting potato flakes from moisture, environmental contamination, and handling damage during storage and transportation.
Before packaging begins, all packaging materials are inspected to ensure they meet internal quality specifications.
Production personnel verify:
- Correct packaging material
- Clean package condition
- Proper package size
- Printing accuracy
- Identificación de lotes
- Production date coding
Only approved packaging materials are released for production.
Standard Packaging Procedure
HJ Potato Flakes uses a structured packaging procedure to maintain product consistency and package integrity.
The process typically includes:
- Filling the designated package with the required product weight.
- Removing excess air from the inner package.
- Sealing the inner liner securely.
- Folding and sealing the outer kraft paper bag.
- Performing weight verification.
- Transferring the finished package to metal detection.
This standardized procedure helps reduce handling variation while protecting product quality throughout distribution.
Packaging Materials
Finished potato flakes are packed using food-grade packaging materials suitable for dehydrated food ingredients.
The standard package consists of:
- Food-grade composite inner liner
- Multi-layer kraft paper outer bag
This packaging structure helps provide:
- Moisture protection
- Mechanical strength
- Product cleanliness
- Stable transportation performance
- Long-distance shipping reliability
Packaging materials are stored under controlled conditions before use to minimize contamination risks.
Weight Control
Accurate Package Weight Verification
Package weight consistency is important for both customer satisfaction and production control.
Each packaging machine is adjusted according to the specified package size before production begins.
For standard industrial packaging, the target filling weight is:
25 kg ± 20 g
Electronic weighing equipment continuously verifies package weight during production.
If weight falls outside the established tolerance, corrective adjustments are made before production continues.
Weight verification records become part of the batch production documentation.
Date Coding and Product Identification
Maintaining Accurate Production Records
Every finished package receives production identification that supports complete traceability.
The coding system typically includes:
- Fecha de producción
- Identificación de lotes
- Production shift
- Product identification
Date coding follows standardized operating procedures.
Whenever the production date changes or printing equipment requires adjustment, production personnel perform verification before continuing normal operation.
Supervisors and Quality Control personnel confirm the accuracy of revised coding information to prevent labeling errors.
Batch Traceability System
Every Batch Has a Manufacturing History
One of the most important principles of modern food safety management is traceability.
Every finished package should be traceable back through the complete manufacturing process.
HJ Potato Flakes maintains production records linking finished products with the corresponding manufacturing information.
Typical traceability records include:
- Approved raw material supplier
- Incoming inspection records
- Fecha de producción
- Production shift
- Processing equipment
- Critical process parameters
- Registros de control de calidad
- Información sobre el embalaje
- Metal detector verification
- Warehouse storage location
- Shipment records
This documentation allows rapid identification of production history whenever customer inquiries, quality reviews, or product investigations are required.
Benefits of Complete Traceability
A comprehensive traceability system supports both food safety and supply chain management.
It enables manufacturers to:
- Identify production history quickly
- Verify manufacturing conditions
- Support customer quality audits
- Investigate quality deviations efficiently
- Demonstrate production consistency
- Improve inventory management
- Facilitate targeted product recall if ever required
Because every production stage generates documented records, traceability extends from incoming potatoes to finished product shipment.
Good Manufacturing Practices (GMP)
The Foundation Supporting HACCP
HACCP does not operate independently.
Its effectiveness depends on strong prerequisite programs, particularly Good Manufacturing Practices (GMP).
GMP establishes the basic operating environment necessary for safe food production before hazard analysis is applied.
Within the potato flake manufacturing process, GMP supports:
- Higiene personal
- Facility cleanliness
- Equipment sanitation
- Controlled production flow
- Safe material handling
- Proper waste management
- Preventive equipment maintenance
Without these prerequisite programs, HACCP controls cannot function effectively.
Personnel Hygiene
Every employee entering production areas follows documented hygiene procedures designed to minimize contamination risks.
Typical hygiene requirements include:
- Clean protective clothing
- Hair restraints
- Hand washing before production
- Hand sanitization where required
- Controlled access to production areas
- Removal of personal items that may contaminate products
Personnel receive periodic food safety training to reinforce hygiene awareness and operational responsibilities.
Equipment Cleaning and Sanitation
Maintaining Hygienic Processing Conditions
Food processing equipment must be cleaned regularly to maintain efficient operation and reduce contamination risks.
Cleaning procedures are established for production equipment including:
- Washers
- Peelers
- Conveyors
- Slicers
- Blanchers
- Cookers
- Mashers
- Drum dryers
- Packaging equipment
Cleaning schedules are developed according to equipment usage, production planning, and sanitation requirements.
Documented cleaning activities help verify that equipment remains suitable for food production.
Production Environment Management
A hygienic manufacturing environment supports consistent food safety performance.
Routine environmental management includes:
- Cleaning production floors
- Waste removal
- Drainage maintenance
- Air circulation management
- Equipment housekeeping
- Separation of waste materials
- Controlled movement of raw and finished products
These practices reduce the possibility of cross-contamination during production.
Waste Management
Controlled Handling of Processing By-products
Potato processing naturally generates by-products such as:
- Potato peel
- Defective potatoes
- Trimmed potato tissue
- Process residues
These materials are separated immediately from food production areas.
Collection points are clearly designated to prevent accidental mixing with finished products.
Where permitted by applicable regulations, certain potato processing residues may be transferred for agricultural utilization, helping reduce waste while maintaining hygienic production conditions.
Preventive Equipment Maintenance
Reliable equipment performance is an important component of food safety.
Preventive maintenance programs reduce unexpected equipment failures that could affect product quality or production efficiency.
Maintenance activities typically include:
- Mechanical inspection
- Lubrication according to food-grade requirements
- Component replacement
- Calibration verification
- Operational testing
Maintenance records provide additional documentation supporting HACCP verification.
Formación del personal
Building Food Safety Awareness
A HACCP system depends not only on equipment but also on trained personnel.
Employees involved in production receive training appropriate to their responsibilities.
Training topics typically include:
- HACCP principles
- Food safety awareness
- Personal hygiene
- Equipment operation
- Prevención de la entrada de materiales extraños
- Cleaning procedures
- Requisitos de documentación
- Medidas correctivas
- Trazabilidad del producto
Continuous training helps maintain consistent implementation of standardized operating procedures throughout the facility.
HACCP Verification and Continuous Improvement
A HACCP system is not static.
Its effectiveness depends on continuous verification and ongoing improvement.
HJ Potato Flakes regularly reviews production data, monitoring records, inspection results, equipment performance, and corrective action reports to confirm that preventive controls continue to operate as intended.
Las actividades de verificación pueden incluir:
- Review of CCP monitoring records
- Internal quality inspections
- Equipment calibration
- Magnet strength verification
- Metal detector performance testing
- Process parameter review
- Batch documentation audits
- Trend analysis of production data
Whenever opportunities for improvement are identified, operating procedures are updated, employees receive additional training when necessary, and corrective actions are documented to strengthen the overall food safety management system.
HACCP Is More Than a Certification
At HJ Potato Flakes, HACCP is implemented as a practical, process-driven management system rather than simply a certification requirement.
From supplier approval and raw potato inspection to thermal processing, moisture control, magnetic separation, metal detection, packaging, and traceability, every stage contributes to a comprehensive preventive food safety strategy.
By integrating scientific process control, documented operating procedures, employee training, equipment verification, and continuous monitoring, we strive to deliver dehydrated potato ingredients that meet the expectations of food manufacturers, industrial processors, and international customers seeking consistent quality, reliable supply, and transparent manufacturing practices.
Scientific Principles Behind Our HACCP Controls
A Hazard Analysis and Critical Control Point (HACCP) system is most effective when preventive controls are based on scientific principles rather than routine inspection alone.
Throughout the potato flake manufacturing process, each control measure is designed to manage a specific food safety or quality risk using validated processing parameters and documented operating procedures.
Rather than relying on finished product testing as the primary safeguard, our manufacturing philosophy emphasizes prevention, continuous monitoring, and process verification throughout production.
The following sections explain the scientific purpose behind several important processing controls used in potato flake manufacturing.
Why Multiple Washing Steps Are Necessary
Fresh potatoes are harvested directly from agricultural fields and naturally carry soil, sand, stones, and plant debris.
A single washing operation cannot reliably remove every contaminant.
For this reason, washing is performed at multiple stages throughout production.
The first washing stage removes heavy field contaminants before peeling.
Post-peeling washing removes loosened skin fragments.
Additional water handling systems help transport potatoes while continuously separating unwanted materials from the product stream.
Using multiple washing stages significantly reduces physical contamination before potatoes reach thermal processing.
Why Steam Peeling Is Preferred Over Conventional Mechanical Peeling
Steam peeling offers several advantages over abrasion-only peeling methods.
High-pressure steam rapidly heats only the outer potato skin.
As pressure is released, the skin separates naturally from the potato surface with minimal removal of edible tissue.
This process improves:
- Raw material yield
- Peeling efficiency
- Consistencia del producto
- Surface cleanliness
- Downstream processing stability
Because less edible potato tissue is removed, steam peeling also contributes to improved production efficiency and more consistent finished product quality.
Why Blanching Is Essential Before Cooking
Blanching is often misunderstood as an initial cooking step.
In reality, its primary purpose is biochemical rather than culinary.
Fresh potatoes contain naturally occurring enzymes that remain active after harvest.
Without blanching, these enzymes may continue to function during processing, leading to:
- Enzymatic browning
- Color deterioration
- Reduced storage stability
- Increased product variation
Controlled blanching deactivates these enzymes while beginning the starch transformation process and preparing potato tissue for uniform cooking.
Why Controlled Cooling Improves Rehydration
Cooling immediately after blanching may appear unnecessary, yet it serves several important technological purposes.
Gradual cooling allows potato cell membranes to stabilize before final cooking.
This helps preserve cellular structure, reduce free starch on the potato surface, and improve the texture of the finished mashed potato after rehydration.
The result is potato flakes that produce a lighter, smoother mash with reduced stickiness and improved water absorption.
Why Gentle Mashing Produces Better Potato Flakes
One common misconception is that finer grinding always produces better potato flakes.
In fact, excessive mechanical force damages potato cells.
Premium potato flakes are produced by gently separating cooked potato tissue while preserving as many intact potato cells as possible.
Maintaining cell integrity improves:
- Natural texture
- Creamy mouthfeel
- Uniform rehydration
- Reduced paste formation
- Consistent product appearance
This is one of the key technical differences between high-quality potato flakes and lower-grade dehydrated potato products.
Why Moisture Control Is More Important Than Drying Temperature
Many people assume higher drying temperatures automatically produce better dehydration.
In reality, finished moisture content is the more important quality indicator.
Excess moisture may shorten shelf life, while excessive drying can damage flavor, color, and texture.
For this reason, drum drying is continuously adjusted by controlling several variables simultaneously, including:
- Steam pressure
- Temperatura del tambor
- Velocidad de rotación del tambor
- Product film thickness
- Feed rate
These parameters work together to achieve stable finished moisture while protecting the natural characteristics of the potato.
Why Magnetic Separation Alone Is Not Enough
Magnetic separators effectively capture ferrous metal particles.
However, they cannot detect every possible foreign material.
For this reason, magnetic separation functions as one layer within a comprehensive physical hazard control system.
Additional protective measures include:
- Extracción de piedras
- Lavado
- Manual inspection
- Tamizado
- Equipment maintenance
- Final metal detection
Using multiple independent barriers provides significantly greater protection than relying on a single inspection step.
Why Metal Detection Is the Critical Control Point (CCP)
Within our HACCP plan, finished product metal detection is designated as the Critical Control Point because it represents the final opportunity to identify metallic contamination before products enter finished goods storage and distribution.
Unlike earlier preventive controls, the CCP requires documented verification at defined intervals using certified metal test pieces.
If verification does not meet established requirements, production is stopped, affected product is isolated, corrective actions are implemented, and the equipment must successfully pass re-verification before production resumes.
This systematic approach helps ensure that the effectiveness of the CCP is continuously confirmed throughout production.
HACCP Monitoring Records
An effective HACCP system depends on accurate and complete documentation.
Production records provide objective evidence that preventive controls have been implemented according to established procedures.
Typical HACCP-related records maintained during potato flake manufacturing include:
| Record Type | Objetivo |
|---|---|
| Raw Material Receiving Records | Verify incoming potato quality and supplier approval |
| Production Batch Records | Document production history and processing conditions |
| Equipment Inspection Records | Confirm equipment operates correctly |
| Steam Pressure Records | Verify thermal processing parameters |
| Blanching Temperature Records | Monitor enzyme inactivation conditions |
| Cooking Time Records | Verify complete thermal processing |
| Drum Drying Records | Monitor moisture control parameters |
| Magnetic Separator Inspection Logs | Verify magnetic strength and cleaning frequency |
| Metal Detector Verification Records | Demonstrate CCP compliance |
| Packaging Weight Records | Confirm package accuracy |
| Product Traceability Records | Link finished products to manufacturing history |
| Corrective Action Reports | Document deviations and resolution |
Maintaining complete records supports internal verification, customer audits, regulatory inspections, and continuous process improvement.
HACCP Prerequisite Programs Supporting Food Safety
The HACCP plan is supported by a series of prerequisite programs that establish the environmental and operational conditions necessary for safe food production.
These programs work together to reduce the likelihood of hazards before critical control measures are applied.
| Prerequisite Program | Primary Objective |
|---|---|
| Good Manufacturing Practices (GMP) | Personnel hygiene and production discipline |
| Procedimientos operativos estándar de higiene (SSOP) | Cleaning and sanitation control |
| Preventive Maintenance | Reliable equipment performance |
| Calibration Program | Measurement accuracy |
| Programa de homologación de proveedores | Uniformidad de la materia prima |
| Pest Management | Facility protection |
| Personnel Training | Consistent HACCP implementation |
| Trazabilidad del producto | Rapid product identification and recall capability |
These prerequisite programs form the operational foundation upon which the HACCP system is built.
Our Commitment to Food Safety
At HJ Potato Flakes, HACCP is integrated into daily manufacturing operations rather than treated as a standalone compliance requirement.
Every stage of production—from receiving fresh potatoes to packaging finished potato flakes—is governed by documented operating procedures, validated processing parameters, equipment verification, sanitation practices, and continuous monitoring.
By combining scientific process control with comprehensive documentation and preventive hazard management, we strive to supply potato flakes and potato powder that meet the expectations of global food manufacturers for safety, consistency, and dependable quality.
Preguntas frecuentes
Q1: Why does HJ Potato Flakes designate final Metal Detection as the absolute Critical Control Point (CCP)?
Because it represents the definitive, non-redundant safeguard before products enter the logistics chain. Our inline digital metal detectors are calibrated to catch tiny remnants (Ferrous ≤1.5mm, Non-Ferrous ≤2.4mm, Stainless Steel ≤3.0mm). System functionality is checked every 4 hours using certified validation test pieces, and any alarm triggers an immediate automated line-isolation protocol.
Q2: How do your dual-layer magnetic separators support the final CCP?
Magnetic separation serves as a crucial preventive upstream barrier. Positioned right after particle size classification, our 8,000 Gauss high-strength magnetic rods capture ferrous equipment-wear microparticles before packaging. We pull and clean these rods every 4 hours and recalibrate their Gauss strength every 10 days, heavily reducing the physical hazard load before the product ever reaches the final metal detector.
Q3: How does your thermal processing parameters explicitly guarantee microbiological safety?
Our core thermal loop features two high-heat steps: industrial steam peeling at 0,8–1,5 MPa and pressurized cooking at 92–99 °C for up to 45 minutes. This dual thermal kill validation effectively neutralizes pathogens associated with raw agricultural root crops, transitioning the raw mash into a highly stable pasteurized state prior to dehydration.
Q4: Can Hongji provide comprehensive batch records for our global trace audits?
Absolutely. Driven by our fully integrated supply chain, every bag is code-stamped to tie back to a complete batch manufacturing record. This allows us to instantly trace the product’s entire lifecycle—from the exact contract farming crop delivery log, water/steam parameter charts, and hourly quality lab sheets, all the way to shipping container numbers.